Overview of the MILLERMATIC 200
The MILLERMATIC 200 is a versatile, high‑speed milling machine designed for precision metalworking. It features a 200 mm work envelope, 3‑axis CNC control, and integrated coolant system. The machine offers rapid tool changes, high spindle speeds up to 12,000 rpm, and a robust safety cage for industrial use.
Model and Serial Information
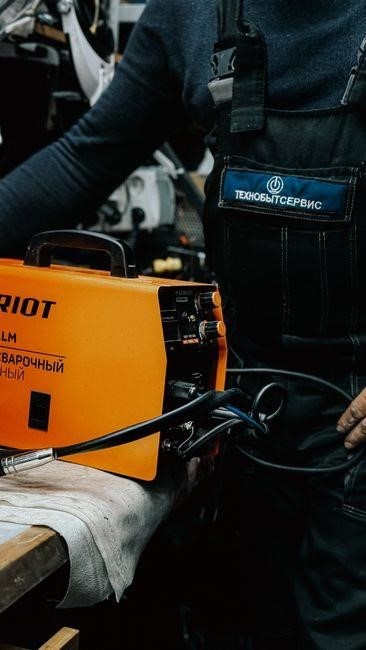
Model: MILLERMATIC 200. Serial Number: Located on the front panel beneath the control board, engraved in a recessed area. The serial is a 10‑digit alphanumeric code that uniquely identifies each unit. It is also printed on the machine’s service label and the original purchase documentation. For warranty and support, provide the full serial string. The serial number is critical for firmware updates, part replacement, and maintenance logs. It ensures traceability and compliance with industry safety standards. The machine’s model designation, MILLERMATIC 200, indicates the 200 mm work envelope and the standard 3‑axis CNC configuration. The model name is stamped on the machine’s frame and appears on the user manual’s cover page. When contacting technical support, reference both the model and serial to receive accurate assistance. The serial number also links to the manufacturer’s database for service history. Always verify the serial before performing any major repair or upgrade. Failure to do so may result in incorrect parts or firmware incompatibility. Keep the serial number in a secure, accessible location for future reference. The serial identifier facilitates compliance audits and ensures that all maintenance actions are traceable. Store the serial in a secure log update it whenever machine is moved or recommissioned.!!
Key Features and Specifications
The MILLERMATIC 200 offers a 200 mm square work envelope, 3‑axis CNC control, and a 12,000 rpm spindle. Its lightweight aluminum frame supports 100 kg, while the integrated coolant system maintains temperature for long runs. Rapid tool change (RTC) with a 3‑position turret allows up to 12 tools per cycle. A built‑in 5‑axis probe enables automatic part registration, reducing setup time. The 7‑inch color touchscreen provides intuitive navigation and real‑time monitoring of spindle speed, feed rate, and tool life. Firmware updates via USB keep the machine current. Safety features include an interlocked cage, emergency stop, and lockout during tool changes. Power consumption is 3 kW, suitable for medium‑size workshops. Dimensions: 1.2 m × 1.0 m × 1.5 m; weight: 350 kg. Compliance: IEC 60204‑1, CE.
- Spindle speed: 0–12,000 rpm
- Axis travel: 200 mm each
- Feed rate: 0–300 mm/min
- Tool capacity: 12 tools
- Coolant flow: 10 L/min
- Power: 3 kW, 230 V, 50 Hz
- Weight: 350 kg
- Dimensions: 1200 mm × 1000 mm × 1500 mm
- Safety: Interlocked cage, emergency stop, lockout during tool changes
- Compliance: IEC 60204‑1, CE
Software integration is achieved via standard G‑code and the proprietary MILLERMATIC Control Suite, offering toolpath optimization, collision detection, and real‑time simulation. The machine supports Ethernet, USB, and serial communication for seamless shop floor integration. All features are documented in the user manual!
Safety Precautions
Ensure the machine is powered down before maintenance. Keep the work area clear of debris and wear proper PPE. Follow lockout‑tagout procedures when servicing. Never bypass safety interlocks or operate the spindle with the guard removed. Report any malfunctions immediately. Follow safety rules!!!.
General Safety Guidelines
Before operating the MILLERMATIC 200, verify that all guards, interlocks, and emergency stops are functional. Keep the machine area free from flammable materials and ensure proper ventilation. Wear safety glasses, hearing protection, and insulated gloves when working with the spindle or coolant system. Never bypass safety devices, and always lock out the machine during maintenance or tool changes. Follow the manufacturer’s recommended torque settings for all fasteners to prevent loosening during operation. Use only approved tooling and maintain proper tool alignment to avoid deflection or vibration. Monitor coolant levels and replace filters regularly to maintain effective cooling and prevent overheating. Inspect the machine for wear or damage before each use, and report any abnormalities to the maintenance team. Adhere to local electrical codes and use a grounded power supply. Keep the machine’s floor clean and dry to prevent slips, and install anti‑trip mats if necessary. Observe all signage and safety instructions posted on or near the machine. Train all operators on emergency shutdown procedures and the proper use of personal protective equipment. Maintain a clear line of sight to the spindle and avoid standing directly in front of the machine while it is running. Ensure that the machine’s emergency stop button is easily accessible and that all operators know its location. Finally, conduct regular safety audits to confirm compliance with industry standards and to identify potential hazards before they become incidents. All personnel must receive formal safety training before operating the MILLERMATIC 200; The machine’s emergency stop should be tested monthly to ensure reliability. Operators should keep a log of any incidents or near‑misses and submit it to the safety officer. The facility should have a fire suppression system rated for metalworking environments. In case of a coolant leak, the area must be isolated and the leak source repaired immediately. The machine should be inspected for electrical continuity and grounding integrity at least once per quarter. Use only the recommended lubricants specified in the maintenance manual to avoid contamination. Ensure that the machine’s enclosure is properly sealed to prevent dust ingress. Maintain a clean workbench to reduce the risk of accidental tool loss. The operator should avoid wearing loose clothing or jewelry that could become entangled. The machine’s vibration levels should be monitored and kept within specified limits to prevent wear. All safety signage should be updated annually to reflect any changes in procedures. The facility should conduct a risk assessment before any major modifications to the machine. The operator should be trained on how to perform a safe shutdown in case of an emergency. The machine’s maintenance schedule should be strictly followed to avoid unexpected failures. The operator should keep a spare set of critical spare parts on hand for quick repairs. The machine’s documentation should be stored in a secure location and be easily accessible to authorized personnel. The safety officer should review all safety protocols quarterly to ensure ongoing compliance. Finally, a comprehensive safety audit should be conducted annually to verify that all safety measures are effective and up to date.
Electrical Safety Requirements
All electrical connections to the MILLERMATIC 200 must conform to the latest IEC 60204‑1 standard. The machine’s power supply should be a dedicated 480 V three‑phase circuit with a minimum 30 A breaker and a 30 A residual‑current device (RCD). All conductors must be sized according to the current rating of the motor and the length of the run, using the manufacturer’s cable tables. The main power cord must be UL‑listed and equipped with a 3‑pole disconnect switch located within 1 m of the machine. Grounding is mandatory: the chassis, coolant reservoir, and any metal housings must be bonded to the earth via a 4 mm² copper conductor. The grounding electrode system should be inspected annually for corrosion or looseness. All control circuits must be isolated from the power supply by a 30 mA RCD. The control panel should include a lock‑out tag‑out (LOTO) device that can be engaged by any operator. Wiring trays and conduits must be rated for the ambient temperature of the workshop and protected against mechanical damage. The machine’s internal wiring should use 4 mm² copper for the motor supply and 2 mm² for control signals. All junction boxes must be sealed and labeled with the machine’s serial number. The emergency stop button must be wired to trip the main breaker and the RCD simultaneously. During maintenance, the power must be isolated using a lock‑out device and verified with a voltage tester before any work is performed. The operator must wear insulated gloves rated for 480 V during electrical work.
Installation Requirements
Place the MILLERMATIC 200 on a level, vibration‑free surface. Ensure a 480 V three‑phase supply with 30 A breaker and RCD. Install a dedicated grounding bus, secure all fasteners, and verify clearance for operator access and coolant flow.
Check grounding.
Site Preparation and Layout
Before installing the MILLERMATIC 200, verify that the work area is level, vibration‑free, and compliant with the machine’s footprint of 1.2 m × 1.5 m. The floor must support a minimum load of 2 kN/m² and be free of cracks or unevenness that could affect spindle accuracy. Provide a 0.5 m clearance on all sides for operator access, tool storage, and emergency egress. Install a dedicated 480 V, 3‑phase power supply with a 30 A circuit breaker, and ensure a separate RCD protects the machine. A grounding bus bar should be connected to the machine chassis and the building’s earth electrode to eliminate stray currents. Place the coolant reservoir 1 m away from the machine, with a drainage system that prevents water accumulation on the floor. Install a dust extraction inlet at the rear of the machine and a dust collector within 2 m to maintain a clean work environment. The machine’s control panel must be positioned 1.2 m above the floor, with a clear line of sight to the operator. Ensure that the machine’s vibration isolation pads are correctly seated and that the surface is free of debris. Finally, test the electrical supply for voltage stability and verify that the RCD trips at 30 A to confirm proper protection.
Ensure the machine’s vibration isolation pads are seated on a concrete slab with shear strength ≥30 MPa. Use a laser level to confirm table flatness within ±0.01 mm. Insulate coolant piping with 50 mm foam to prevent floor condensation, and seal dust ducts with flexible metal sleeves. Record all data. Align
Power Supply and Wiring
The MILLERMATIC 200 requires a dedicated 480 V, 3‑phase, 60 Hz supply with a minimum current rating of 30 A per phase. The main circuit must be protected by a 30 A, 480 V, 3‑phase circuit breaker located within 3 m of the machine. A separate 20 A, 480 V, 3‑phase breaker should feed the machine’s control panel, ensuring isolation between the drive and control circuits. All wiring should use 4 AWG copper conductors for the main power feed and 12 AWG for the control circuits, with appropriate insulation (XLPE or THHN) rated for 90 °C. The neutral and earth conductors must be bonded at the main disconnect and at the machine’s grounding bus bar. A 30 A residual‑current device (RCD) must be installed on the main supply to provide protection against earth‑fault currents. The control panel’s power input should be connected to a 120 V, 60 Hz single‑phase supply, with a 15 A circuit breaker. All connections must be tightened to the manufacturer’s torque specifications (typically 0.8 Nm for 4 AWG, 0.4 Nm for 12 AWG). Wire routing should avoid sharp bends and be secured with cable ties every 0.5 m. Ground fault monitoring should be enabled on the machine’s PLC, and a dedicated ground fault circuit interrupter (GFCI) should be installed on the control panel to trip within 30 ms of a fault. The machine’s power cable must be rated for 480 V, 3‑phase, 60 Hz, and should be routed through a cable gland that provides a tight seal against dust and moisture. All junction boxes and splice points must be enclosed in a weather‑proof, fire‑resistant enclosure with a minimum IP65 rating. The power supply should be tested with a calibrated clamp meter before commissioning, verifying that voltage and current draw are within specified limits. Finally, a maintenance log should record the date of installation, the breaker numbers, and the results of the initial power‑on test. This ensures traceability and compliance with safety regulations. All electrical work must be performed by a licensed electrician in accordance with local codes and the manufacturer’s guidelines. Regular inspection of the wiring harnesses and connectors is recommended to prevent corrosion and ensure long‑term reliability.
Operating Instructions
Before use, set spindle speed, and power on the machine. Load the program via the touch‑screen interface, then use jog controls for manual positioning. Monitor spindle temperature. When finished, shut down the spindle, secure the workpiece. Follow safety signs. PPE!!
The MILLERMATIC 200 is a versatile, high‑speed milling machine designed for precision metalworking. It features a 200 mm work envelope, 3‑axis CNC control, and integrated coolant system. The machine offers rapid tool changes, high spindle speeds up to 12,000 rpm, and a robust safety cage for industrial use.
Machine Controls and Interface
The MILLERMATIC 200 employs a dual‑mode control system that combines a high‑resolution touch screen with a joystick for manual operation. The touch panel, located on the front console, displays real‑time machine status, spindle speed, feed rate, and tool position in a customizable layout. Users can load G‑code files via USB or Ethernet, edit parameters directly on the screen, and execute programs with a single button. The joystick, mounted on the control cabinet, offers eight‑way movement and a dedicated “Jog” mode for fine‑tuned adjustments. Each axis has a separate speed dial, allowing operators to set low‑speed precision or high‑speed production speeds. A built‑in LCD monitor shows spindle RPM, tool length, and coolant flow, while audible alarms alert to over‑temperature or tool wear. The interface includes safety interlock buttons that must be pressed before the spindle can be activated, and an emergency stop that cuts power instantly. For users, a port provides access to the machine’s firmware for diagnostics and custom programming. The control panel also features a macro button that can trigger a sequence of movements or tool changes, streamlining tasks. All controls are rated for use and are protected by an enclosure to maintain reliability in shop environments. Operators can customize the interface by rearranging toolbars, setting default feed rates, and saving profiles for workpieces, ensuring high consistency for all users, ensuring safety
Maintenance Procedures
Daily checks include cleaning the spindle, inspecting belts, and verifying coolant levels. Lubricate bearings every 200 hours, replace filters monthly, and update firmware quarterly. Log all actions in the maintenance logbook for traceability. All tasks logged.OK!
Daily Maintenance Checklist
Before each operation, perform the following inspections and cleaning tasks to ensure optimal performance and longevity of the MILLERMATIC 200:
- Spindle and Tool Path: Visually inspect the spindle for any visible debris or wear. Use a lint‑free cloth to wipe the spindle head and surrounding area. Check the tool holder for proper seating and torque.
- Drive Belts and Pulleys: Inspect all belts for cracks, fraying, or excessive slack. Verify pulley alignment by measuring the center‑to‑center distance with a caliper. Tighten or replace belts as needed.
- Coolant System: Confirm coolant reservoir is at the recommended level. Inspect hoses for leaks or kinks. Flush the coolant lines if a buildup of particulates is observed.
- Electrical Connections: Check all terminal blocks for tightness. Look for signs of corrosion on connectors and clean with a contact cleaner if necessary.
- Safety Cage and Guards: Ensure the cage is fully closed and all guards are in place. Verify that the emergency stop function is responsive.
- Documentation: Record the date, time, and any observations in the maintenance log. Note any corrective actions taken and the personnel responsible.
Completing this checklist daily helps prevent unexpected downtime and extends the machine’s service life.
Lubrication and Service Intervals
Lubrication of the MILLERMATIC 200 follows a strict schedule to keep precision high and wear low. Spindle bearings receive a high‑viscosity synthetic grease every 500 hours or when noise appears. Ball‑screw and linear‑guide assemblies are oiled with machine‑oil once per 1,000 hours, ensuring smooth travel. Coolant‑pump bearings get a light oiling every 200 hours to keep pressure stable. All points are in the service panel; use the supplied grease guns and avoid over‑application, which attracts dust. After each service, wipe excess grease from exposed surfaces to prevent buildup on the exterior. Log every lubrication event with hour counter, part serviced, and lubricant type. Following these intervals reduces downtime, preserves accuracy, and extends component life, matching the manufacturer’s recommendations for reliability.
Periodic checks of the spindle drive occur every 250 hours. Inspect gear mesh for wear, verify spindle mounting torque, and replace worn teeth per the manual. Coolant filter should be inspected and replaced every 600 hours to avoid contamination. When servicing, flush lines with clean water and re‑add coolant at the correct concentration. Visual inspection of bearing housings for leakage or discoloration is essential; abnormal findings trigger immediate replacement. Documenting these activities ensures traceability and supports preventive maintenance planning.
Routine checks of the coolant filter and pump seals are recommended every 300 hours. Replace any worn seals to maintain proper coolant flow and avoid overheating. Additionally, inspect the machine’s safety cage and emergency stop function daily; any malfunction should be corrected before the next run. These small actions collectively safeguard the machine’s longevity and performance.Also
Troubleshooting Guide
When the MILLERMATIC 200 encounters problems, follow these steps to isolate and resolve the issue. 1. Spindle Vibration: Check the spindle bearing for wear. If the vibration persists after lubrication, replace the bearing kit. 2. Coolant Flow: Verify the coolant pump is operating. A drop in pressure indicates a clogged filter or a failing pump seal; replace the filter or seal accordingly. 3. Error Code 0xA1: This indicates a limit switch fault. Inspect the switch contacts for corrosion and clean with isopropyl alcohol. 4. Power Loss: Ensure the 480 V supply is stable. A voltage drop below 470 V triggers a shutdown; check the transformer and main breaker. 5. Tool‑Change Failure: If the tool‑change stalls, inspect the cylinder for leaks and refill the reservoir. 6; Control Panel Display Off: Reset the PLC by cycling the main power. If the display remains blank, replace the control board. 7. Unusual Noise: A whining noise may signal a misaligned ball screw. Tighten the ball‑screw bolts to the specified torque and re‑align the guide rails. 8. Overheating: Monitor spindle temperature; if it exceeds 80 °C, check the cooling fan and replace if necessary. 9. Safety Cage Warning: A warning light indicates a missing safety cover; replace the cover and re‑engage the latch. For persistent issues, contact technical support with the serial number and error logs!!!..